Build the automation ladder before robotic sewing
Robotic sewing should sit near the top of an automation sequence, not at the beginning. Start with work the factory can define, observe, and recover when something goes wrong.
Agree on the method, input condition, quality rule, cycle-time basis, and exception owner.
Locate work in progress (WIP), defects, downtime, rework, and changeover delay before buying advanced equipment.
Test cutting control, material movement, inspection assistance, or one stable bottleneck with a manual fallback.
Limit the trial to a named operation, fabric range, style range, changeover rule, and recovery plan.
Move up one rung only when four conditions are visible
- Repeatable input: the material, operation, and handoff vary within a known range.
- Measured loss: the factory can show the delay, defect, handling, or labor problem being reduced.
- Acceptance rule: production and quality teams agree on what counts as a usable result.
- Recovery owner: someone can stop, bypass, maintain, and restart the process without hiding disruption elsewhere.
Boundary: This ladder does not mean every factory must reach robotic sewing. The useful endpoint may be better cutting control, visible WIP, assisted inspection, or safer material movement.
The wrong automation question is: which robot should we buy?
The better question is: which factory problem is stable, measurable, and valuable enough to automate first?
For garment factories, automation should begin with process readiness. Without clean data, visible WIP, clear quality standards, and maintenance capability, even advanced equipment can become an expensive experiment. This is especially true in apparel, where soft fabric, style changes, line balancing, and quality judgment make full robotic sewing harder than it looks.
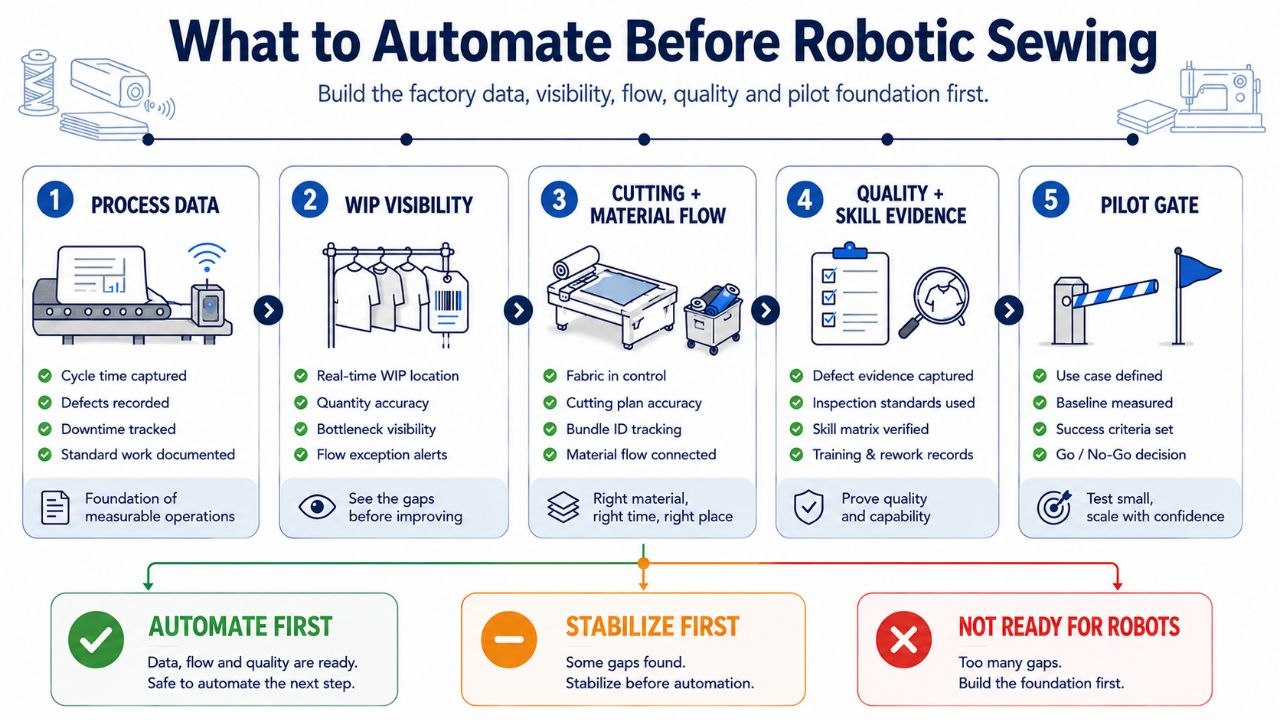
A practical garment factory automation roadmap should start before the sewing robot.
1. Start with process data, not robots
A factory cannot automate what it cannot define.
Before buying machines, the factory should clean up its basic operating data:
- style master
- BOM and material records
- operation breakdown
- SMV or SAM
- line layout
- worker IDs and skill matrix
- defect codes
- material status
- cutting and numbering records
- shipment plan
This foundation is not glamorous, but it decides whether MES, AI inspection, connected machines, and robotics will produce useful results.
If the operation sequence is unclear, the defect code is inconsistent, or WIP is invisible, automation will amplify confusion instead of solving it.
2. Make WIP visible first
The first practical automation layer is often visibility.
QR, barcode, RFID, or MES systems can track cutting issue, sewing input, process output, inline quality, endline output, rework, finishing, packing, and carton status.
For many garment factories, QR or barcode tracking is a better first step than full RFID. It is cheaper, easier to train, and usually enough to expose bottlenecks. RFID can be useful, but it does not automatically create discipline. If scanning is skipped or master data is wrong, the dashboard becomes decoration.
Good WIP visibility should answer practical questions:
- Which line is blocked?
- Which operation is the bottleneck?
- Where is rework accumulating?
- Which bundle or carton is delayed?
- Which style is at shipment risk?
3. Improve cutting before chasing robotic sewing
Cutting-room automation is usually more mature than sewing automation.
CAD, marker optimization, auto spreading, automatic cutting, defect mapping, shade-lot control, numbering, bundling, and cut-panel tracking can produce measurable benefits before full robotic sewing.
Fabric cost is a major part of garment cost. Better marker efficiency, spreading quality, shrinkage control, and cutting accuracy can reduce waste and prevent downstream sewing problems.
A weak cutting process creates rework and line disruption later. A stronger cutting process gives sewing automation a better foundation.
Vendor product pages may claim large improvements in speed or fabric utilization. Those claims should be treated as vendor claims, not universal guarantees. The factory still needs to check fabric type, order mix, marker discipline, maintenance, operator training, and real cutting-loss data.
4. Use AI inspection where criteria are clear
AI inspection should start where defect criteria are visible and repeatable:
- fabric defects
- shade bands
- print placement
- embroidery defects
- label position
- logo placement
- trim verification
- carton labels
- packing checks
Do not start with the most subjective final garment judgment. Start with repeatable inspection points where lighting, camera position, standard sample, and accept/reject rules can be controlled.
AI inspection should support QC, not replace final quality judgment. The key questions are not only model accuracy. They are false rejects, escape rate, lighting stability, defect-library quality, and how the result connects to rework, CAPA, and shipment decisions.
5. Digitize skills and work instructions
Operator skill variation is one of the main reasons garment automation is difficult.
Digital work instructions, operation videos, defect libraries, and skill matrices can reduce ramp-up time and make line balancing more reliable. This is especially important when factories introduce connected machines, templates, or new equipment.
A machine is only as useful as the operator and supervisor routines around it. If supervisors, mechanics, and operators do not know how to maintain the process, the automation cell will not stay stable.
6. Automate bottleneck operations before full sewing lines
After WIP and quality data are visible, the factory can identify real bottlenecks. This is the right time to consider targeted equipment:
- template sewing
- programmable pattern sewing
- pocket setters
- label machines
- bartack
- buttonhole
- button attach
- hemming
- waistband operations
- selected folding, pressing, or finishing aids
The pilot should be small. Choose one factory area, one or two lines, and a few stable styles. Measure WIP, output per labor hour, rework, changeover time, downtime, and maintenance response.
Do not judge automation only by machine speed. Judge it by line performance.
7. Add connected machines and maintenance data selectively
Connected sewing machines and IoT sensors can help factories see machine utilization, idle time, error codes, thread breaks, cycle counts, and maintenance needs.
The first targets should be critical machines:
- auto cutters
- spreading machines
- embroidery machines
- compressors
- boilers
- special automatic sewing machines
- bottleneck equipment
Putting sensors on every machine may not be the best first investment. Start where downtime stops the floor or creates shipment risk.
8. Consider material-flow robots and logistics automation
In larger factories, material movement can be a better early robotics use case than sewing itself.
AMRs, AGVs, smart carts, warehouse automation, and automated storage systems can move fabric rolls, bundles, trims, cartons, or finished goods. These tasks are often more structured than flexible sewing operations.
The readiness questions are practical:
- Are the aisles wide enough?
- Is the floor condition stable?
- Are traffic rules clear?
- Are loading and unloading points standardized?
- Is there a manual fallback?
- Can the system connect to WMS, MES, or production planning?
- How will worker safety be managed?
Moving materials reliably may be easier to automate than sewing fabric.
9. Use textile sorting and recycling as a structured automation lesson
Textile sorting and recycling are useful examples because the task can often be structured around imaging, classification, and material flow.
Recent public examples include AI-powered garment sorting projects, hyperspectral imaging, and robots that classify used clothing at high speed. These cases do not prove that sewing is easy to automate. They show that apparel-related automation may advance faster when the task is easier to standardize.
For garment factories, the lesson is clear: choose the process where the physical, data, and quality boundaries can be controlled.
10. Define pilot metrics before installation
A good pilot should have clear metrics before installation.
Useful KPIs include:
- WIP days
- bottleneck WIP
- line efficiency
- output per labor hour
- DHU
- rework rate
- cutting loss
- downtime
- changeover time
- operator ramp-up time
- on-time shipment risk
If these metrics are not defined, the factory may only learn that a machine can run. It may not learn whether the factory improved.
Automation-sequencing mistakes to avoid
Common mistakes include:
- buying technology before process mapping
- treating RFID as automatic discipline
- ignoring rework
- installing AI inspection without defect standards
- selecting automatic machines without style-compatibility checks
- failing to train mechanics and supervisors
- using production data as punishment
The last point matters. If workers see automation as surveillance only, trust will decline and data quality will suffer.
Practical roadmap
A practical sequence is:
- Clean master data.
- Make WIP visible.
- Improve cutting.
- Pilot AI inspection where criteria are clear.
- Digitize skills and work instructions.
- Automate bottleneck operations.
- Connect critical machines and maintenance data.
- Test material-flow robots or logistics automation where flow is structured.
- Build AI production alerts from real data.
- Evaluate robotic sewing only where product mix, fabric behavior, changeover, and quality standards are controlled.
This is not the fastest-looking path. It is the path most likely to survive real factory conditions.
Final automation-sequencing takeaway
Garment factories should automate first where the process is stable, the problem is measurable, and the benefit is connected to WIP, quality, cost, or shipment reliability.
The best automation roadmap does not start with the most impressive robot. It starts with the factory problem that is ready to be solved.
About the Editorial Perspective
Factory AI Atlas is written from a manufacturing operations perspective shaped by hands-on apparel and textile production experience, including overseas factory management, woven and knit operations, production control, quality systems, and operational restructuring.
The site focuses on vendor-neutral, evidence-aware, and ROI-realistic guidance for AI, robotics, automation, and factory readiness. See the Editorial Policy & Disclaimer for sourcing standards and AI-use disclosure.
Sources checked and what they do not prove
- International Federation of Robotics industrial robot resources — provides broad adoption and application context; it does not show that robotic sewing is ready for a specific fabric, style mix, or factory.
- NIST smart manufacturing resources — supports the importance of measurement, interoperability, and process visibility; it does not define an apparel automation sequence by itself.
- OSHA robotics guidance — supports safety, training, and risk-control planning; it is not a productivity or return-on-investment guarantee.
This article is an editorial operating guide. A real investment decision still needs process data, product trials, safety review, maintenance capability, worker input, and factory-specific acceptance criteria.