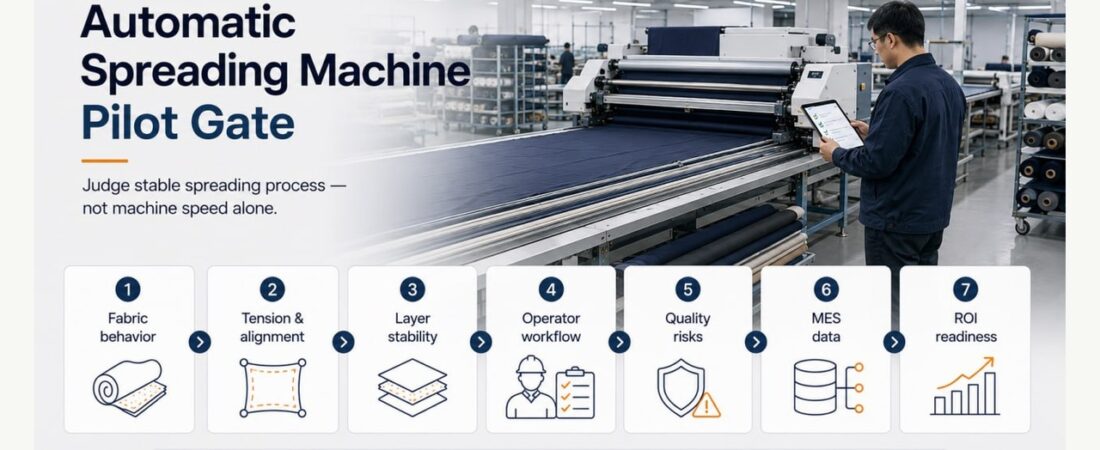
Test the spreading process as a matrix, not a speed demo
An automatic spreader should be tested across the fabric and operating conditions the cutting room actually receives. One fast run on stable material does not show whether the process can protect tension, edge alignment, ply stability, shade control, end loss, and the work that follows spreading.
Include stable woven, stretch knit, slippery or lightweight fabric, face-sensitive material, and any roll condition that regularly needs operator care.
Record relaxation status, roll identity, shade group, ply count, spreading length, table condition, machine settings, and the operator.
Measure edge deviation, tension events, ply movement, speed, end loss, stops, manual corrections, and time—not only maximum machine speed.
Test roll changes, splice handling, fabric faults, emergency stop, restart, short lays, marker changes, and the recovery steps operators must follow.
Review cutting accuracy, shade separation, bundle integrity, rework, and operator feedback before calling the spreading result acceptable.
What the pilot record should show
Keep each fabric condition and machine setting beside its quality result. A useful record links the spread to the cut and bundle outcome, names every intervention, and makes failed conditions visible instead of averaging them into one speed figure.
Boundary: better speed or cleaner machine data does not prove lower total cost. Labor use, end loss, maintenance, calibration, training, safety controls, downstream defects, and production mix still need separate evidence.
Buying an automatic spreading machine should not begin with a speed demonstration. It should begin with a process stability test under real factory conditions.
In many garment factories, the first question about an automatic fabric spreading machine is simple: how fast can it run, and how many operators can it reduce? That question is understandable. Spreading is repetitive, physically demanding, and directly connected to cutting-room productivity.
But speed alone is not a buying test. A machine can look impressive during a vendor demonstration and still create problems when it meets real fabrics, real operators, real quality controls, and real production schedules.
The better way to evaluate automation is to use a Fabric-control pilot gate: a structured test that checks whether the factory can create stable, repeatable spreading quality under actual operating conditions.
This is why the real question is not only whether the machine can run fast. The real question is whether the spreading process is stable enough to support quality, data visibility, operator workflow, and measurable ROI.
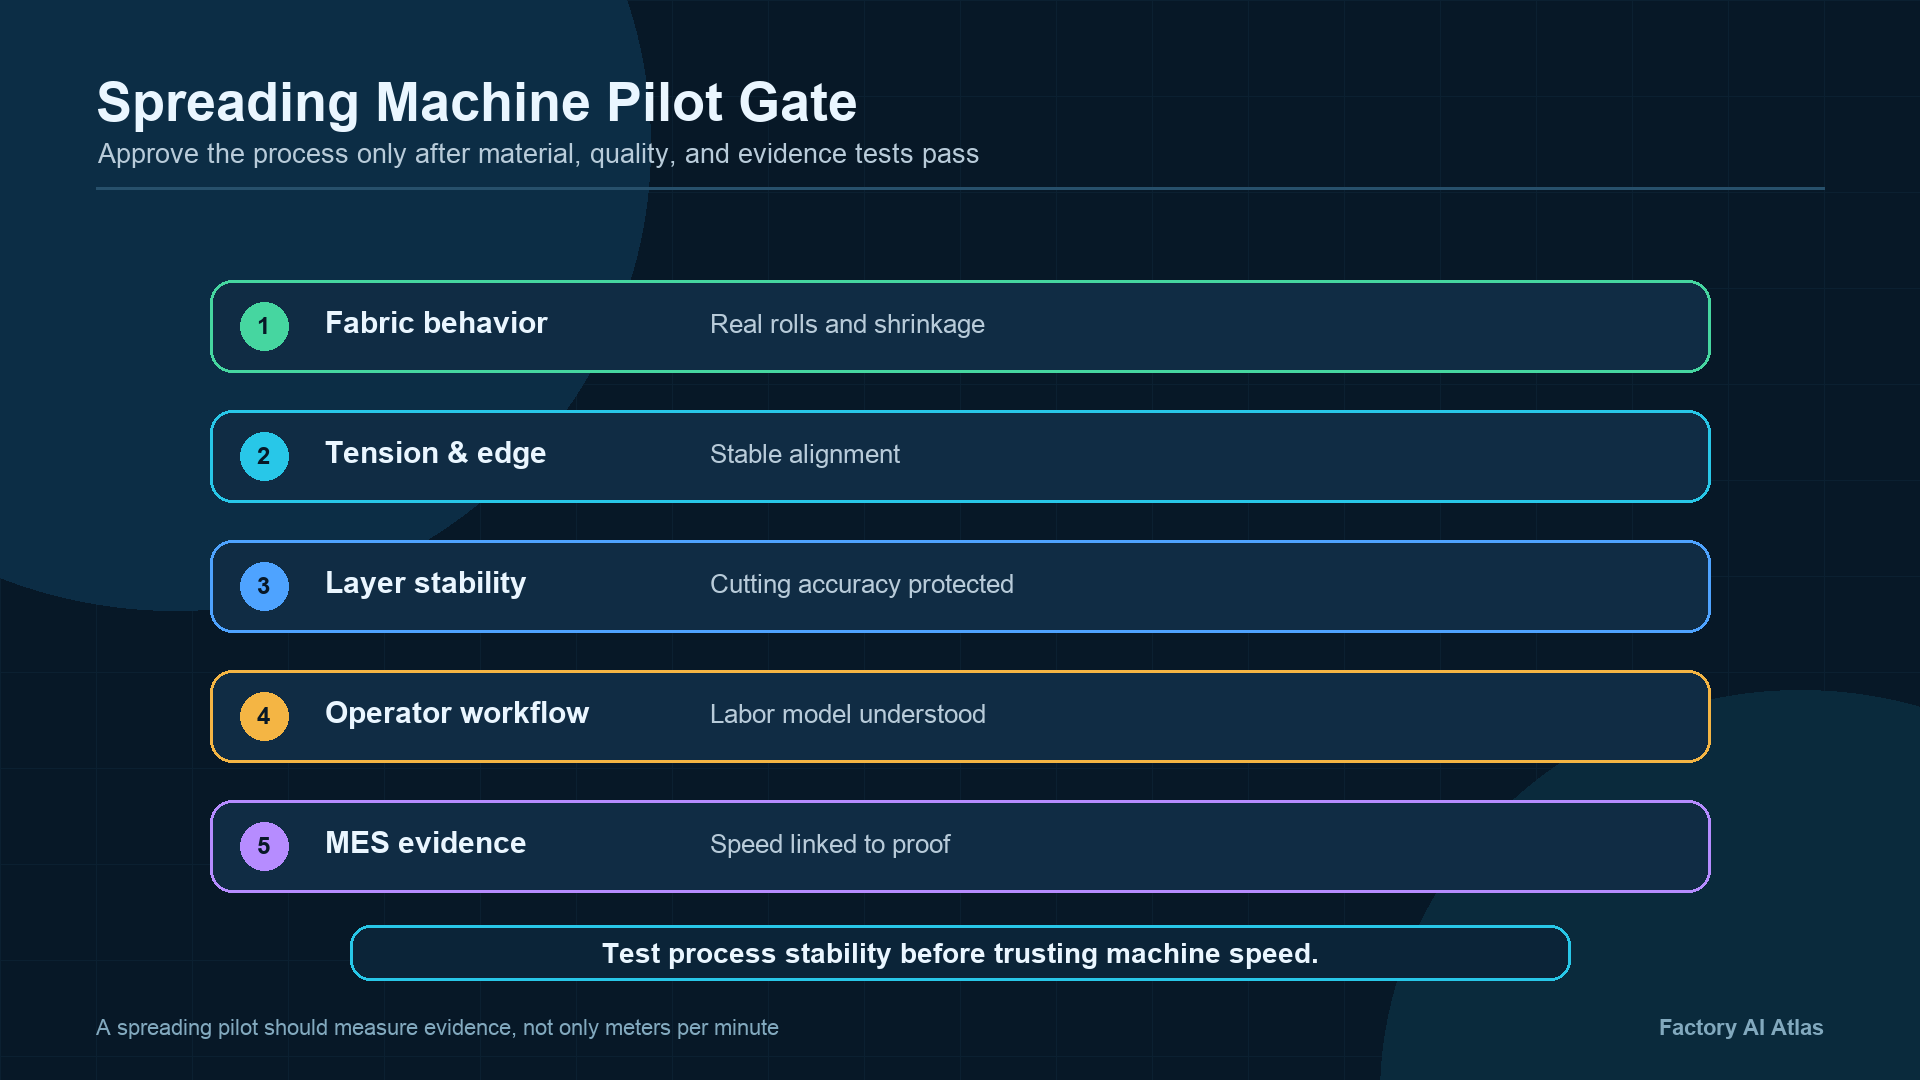
1. Fabric Behavior: Test the Material, Not the Demo
Fabric behavior is the first gate. A spreading machine may perform well on one material and struggle on another. Lightweight jersey, stretch fabric, slippery synthetic fabric, heavy fleece, bulky rolls, unstable selvage, nap direction, and roll tension variation can all change the result.
A serious pilot should not use only the easiest fabric category. It should include the fabric types that expose risk in the real factory order mix.
- Does the fabric relax or curl after spreading?
- Does roll tension change during the table?
- Does the material feed smoothly without distortion?
- Does the machine handle both light and heavy fabric categories?
2. Tension & Alignment: Speed Is Meaningless if the Edge Is Unstable
For cutting-room managers, edge alignment and tension control are more important than headline speed. If fabric edges drift, skew, or stretch during spreading, the problem moves downstream into marker accuracy, cutting quality, and rework.
The pilot should check whether the machine can maintain stable feeding, edge alignment, and tension across the full table length. The test should also record when manual correction is needed.
- Edge alignment across the table
- Fabric skew or bowing
- Tension consistency by fabric category
- Manual intervention count
- Spreading direction and fabric relaxation behavior
3. Layer Stability: Automation Must Protect Cutting Accuracy
Layer stability is where spreading automation becomes a quality decision, not just a productivity decision. A table that looks fast but creates ply shifting, wrinkles, curling, or layer-to-layer inconsistency can increase cutting defects.
The pilot gate should ask whether the spread table is ready for cutting without hidden correction work. If not, automation is only transferring the defect to the cutting stage.
- Ply-to-ply consistency
- Layer shifting during spreading
- Wrinkles or surface waves
- Marker alignment risk
- Cut panel accuracy risk after spreading
4. Operator Workflow: Automation Changes the Labor Model
An automatic spreading machine is not simply a “remove one person” tool. It changes the operator workflow. Roll loading, fabric changeover, exception handling, table preparation, inspection, and supervisor support must all be redesigned.
Many factories want to move from a two-operator model to a one-operator model. That may be possible under defined conditions, but it should be proven through the pilot rather than assumed from the machine brochure.
- Can one operator safely manage normal operation?
- When is a second person still required?
- How difficult is roll loading and changeover?
- What training does the operator need?
- How quickly can supervisors respond to exceptions?
5. Quality Risks: The Risk Does Not Disappear — It Moves
Automation does not remove quality risk by itself. It changes where the risk appears and how quickly the factory can detect it. Tension marks, fabric distortion, shade issues, selvage instability, ply slippage, and hidden rework must be tracked during the pilot.
The goal is not to prove that the machine has no risk. The goal is to identify which risks are reduced, which risks remain, and which risks require process controls.
- Tension marks or fabric distortion
- Shade, nap, or direction issues
- Ply slippage before cutting
- Rework or correction after spreading
- Defect detection and escalation routine
6. MES Data: ROI Needs Process Evidence
Factory AI readiness begins when process evidence becomes visible. If the spreading pilot does not collect useful data, ROI becomes a feeling rather than a calculation.
Even if a factory does not have a full MES integration yet, it should still structure the pilot data: spreading time, downtime, fabric loss, end loss, manual correction, operator input, defect records, and cutting output linkage.
- Spreading time by style and fabric category
- Machine downtime and stop reasons
- Fabric loss and end loss visibility
- Manual correction and exception records
- Connection to order, style, fabric, and cutting output
7. ROI Readiness: The Buying Decision Must Reflect Real Conditions
The final gate is ROI readiness. Labor saving is important, but it is not the whole calculation. A factory should include quality stability, fabric loss reduction, cutting accuracy, rework reduction, utilization rate, training cost, maintenance support, and the actual order mix.
A pilot is useful only when it proves stable quality under real factory conditions. Otherwise, the factory may buy speed without buying reliability.
- Labor saving under realistic operator workflow
- Fabric loss reduction and quality stability
- Training and maintenance cost
- Machine utilization rate across real orders
- Supervisor trust and operator acceptance
Approve stable fabric control before higher speed
The real test of an automatic spreading machine is not machine speed alone. It is whether the factory can run a stable spreading process across fabric behavior, tension and alignment, layer stability, operator workflow, quality risks, MES data, and ROI readiness.
For apparel factories, automation should be purchased only after the real process has been tested — not just the machine.
Evan Lee factory field note
Read speed together with fabric control
An automatic spreading-machine trial should not be judged only by meters per minute. The factory needs to watch fabric relaxation, tension, ply alignment, edge control, roll changes, shade/lot separation, marker sequence, operator intervention, and the effect on cutting quality. Speed without fabric control can simply move defects faster into the next process.
Sources checked and what the pilot must still prove
- OSHA machine guarding guidance — provides a safety baseline for moving equipment, guarding, and operator exposure.
- NIST manufacturing resources — supports connecting equipment data, workforce skills, and shop-floor systems.
- ISO 12100 machinery safety risk-assessment standard — provides a risk-assessment reference for machinery design and use.
These sources do not prove fabric control, spreading quality, operator workload, cutting-room fit, throughput, or return on investment for a specific factory. Those claims require a bounded pilot using the factory’s own fabrics, layouts, operators, quality checks, and downstream records.